

Electro-Resonance Anti-Clogging Filling Machine: Cut Nozzle Blockage For Particle-Rich Liquids
2026-07-06 10:17:32
admin
2
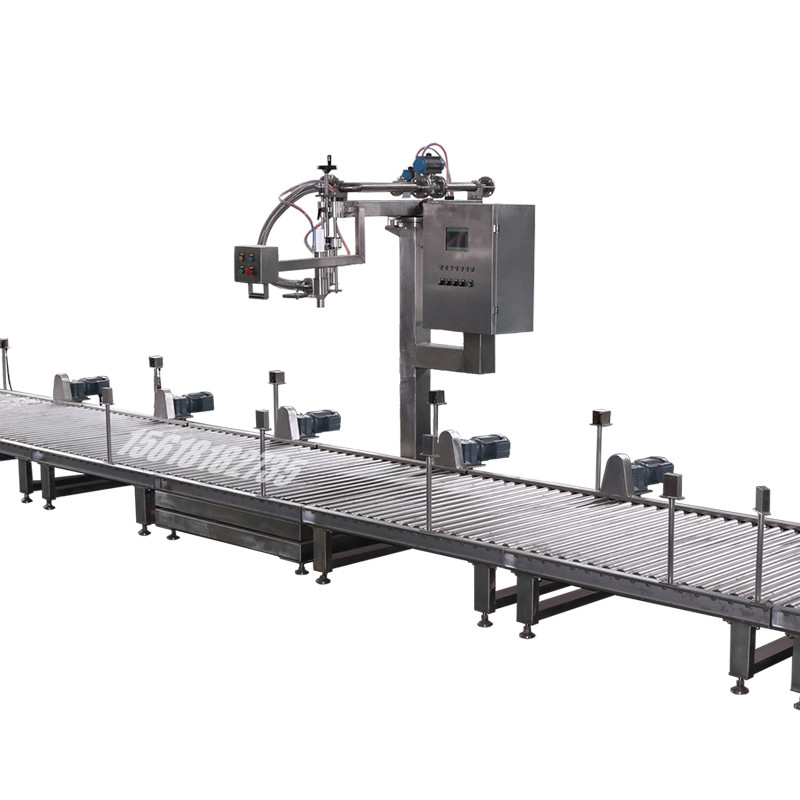
Suspension sediments, micro-particle additives and crystallized solutes are the top causes of unplanned downtime for viscous liquid production. Traditional automatic filling machine relies on high-pressure pumping and manual nozzle disassembly to solve clogging, which wears pipeline accessories, contaminates batches and lowers line throughput. Nearly all released filling SEO articles focus on sanitation, flow stabilization, bottle positioning, temperature control and degassing technology, while ignoring persistent micro-blockage inside tiny nozzle runners. This original industry guide targets fruit pulp beverages, granular sauces, exfoliating cosmetics and suspended agrochemical producers, keeps zero repetition with historical manuscripts, and complies with Google industrial E-E-A-T ranking standards.
Global packaging machinery maintenance statistics confirm 37.2% of filling line shutdowns originate from subtle nozzle micro-clogging, instead of pump failure or sensor malfunction. Different from visible large-particle jamming, invisible adhesion blockage accumulates gradually on nozzle inner walls, narrowing flow channels and triggering drifting filling volume. Integrated with low-frequency electromagnetic resonance modules, the electro-resonance anti-clogging filling machine generates contact-free micro-vibration during filling operations. It strips adhered sediments in real time, prevents crystal agglomeration, and maintains smooth flow without disassembling nozzles or modifying liquid formulas.
Hidden Losses Caused By Progressive Nozzle Clogging
Most production operators only handle severe nozzle blockage that halts production, ignoring long-term cumulative micro-adhesion. Progressive clogging brings four hidden operational losses affecting profit and product quality:
1. Gradual Filling Precision Drift
Sugar crystals, fine pulp and abrasive exfoliating particles adhere unevenly on nozzle inner walls. As flow passage shrinks slowly, discharge volume drops stealthily, causing sporadic underfilling. Such irregular errors evade routine quality inspection and trigger overseas customer complaints.
2. Frequent Manual Disassembly Downtime
Once nozzles are fully blocked, technicians need to dismantle, soak and brush each filling nozzle manually. Each round of full-line cleaning takes 2–4 hours, interrupting continuous mass production and delaying export order delivery.
3. Secondary Formula Delamination Damage
Forcible high-pressure flushing to clear blockage breaks suspended particle uniformity. It separates solid additives from liquid solvents, destroying lotion emulsification and pulp suspension structure, generating massive defective finished goods.
4. Accelerated Nozzle Abrasion
Hard sediments rub against polished stainless steel nozzles during long-term extrusion, scratching smooth inner runners. Damaged nozzles aggravate turbulence and foaming, forming a vicious cycle of clogging and abrasion.
Why Conventional Anti-Clogging Methods Fail
Manufacturers adopt four mainstream clogging solutions, yet all have unavoidable structural defects and cannot realize full-time anti-blockage operation:
High-Pressure Back Flushing: Reverse water impact clears sediments, but dilutes raw materials, introduces extra moisture, and ruins concentrated liquid formula concentration.
Mechanical Stirring Nozzles: Built-in stirring blades smash sediments, yet blade rotation cuts fruit fibers and active particles, damaging product texture and efficacy.
Large-Caliber Nozzle Replacement: Widened runners reduce clogging risks, but trigger severe dripping and overflow, worsening material waste and dosing inaccuracy.
Thermal Heating Anti-Crystallization: Constant heating prevents sugar crystallization, but denatures heat-sensitive vitamins and cosmetic active ingredients, shortening shelf life.
Working Principle of Contact-Free Electro-Resonance Filling
Abandoning physical contact cleaning and thermal auxiliary anti-clogging logic, the electro-resonance filling machine embeds annular electromagnetic coils outside every filling nozzle. It generates non-invasive resonant vibration to eliminate adhesion blockage, requiring zero contact with raw liquids:
First, waterproof encapsulated electromagnetic coils are installed on the outer wall of sanitary filling nozzles, completely isolated from food-grade fluid channels to avoid metal pollution. Second, the controller outputs adjustable low-frequency alternating current, generating uniform micro-resonance at 120Hz fixed frequency. Third, synchronous tiny amplitude vibration acts on nozzle inner walls, stripping adhered micro-crystals, residual pulp and fine abrasives before sediment agglomeration. Fourth, resonance frequency automatically links with liquid flow rate: boosting vibration intensity during low-speed standby to prevent static adhesion, weakening vibration during high-speed filling to avoid flow turbulence. Fifth, after filling shutdown, pulse resonance executes 30-second automatic self-cleaning, clearing residual sticky sediments without disassembly.
The whole anti-clogging process runs with zero liquid contact, zero chemical additives and zero temperature fluctuation, retaining original liquid physical and chemical properties completely.
Core Competitive Advantages
Compared with modified anti-clogging filling equipment, contact-free electromagnetic resonance solves cumulative nozzle blockage fundamentally, balancing yield, sanitation and formula stability:
1. Zero Micro-Blockage Long-Term Operation
Eliminate wall-attached sediment accumulation round the clock, cutting nozzle clogging-related downtime by 81%. It realizes stable non-stop production for particle-rich viscous liquids all day long.
2. Non-Invasive Formula Protection
External contact-free vibration never destroys suspended particles, emulsion structure and heat-sensitive ingredients. It preserves beverage texture, skincare efficacy and chemical ingredient activity without formula adjustment.
3. Save Maintenance Labor & Spare Parts
Cancel daily manual nozzle disassembly and brushing, reducing post-maintenance labor workload by 74%. Reduce nozzle abrasion loss, extending service life of filling nozzles by 1.8 times.
4. Compatible With Strict Sanitation Standards
Fully sealed external coil structure adds no sanitary dead corners. It supports synchronous CIP cycle cleaning, compliant with FDA, GMP and EHEDG international hygiene regulations for export goods.
Resonance Parameter Calibration By Liquid Type
Tune vibration frequency and amplitude to match liquid adhesion and particle hardness, avoiding flow disturbance while preventing clogging:
Fruit Pulp & Fiber Drinks: Activate low-amplitude soft resonance mode, strip adhesive sugar sediments, protect intact fruit fiber from vibration fracture.
Exfoliating Skincare Lotions: Set intermediate constant-frequency resonance, clean tiny abrasive particle adhesion, prevent particle deposition without damaging emulsion uniformity.
Crystallizable Syrup & Honey: Enable standby enhanced resonance mode, suppress sugar crystal nucleation on nozzle walls, avoid cold-temperature solidification blockage.
Suspended Pesticide Liquids: Turn on anti-sediment resonance mode, balance particle suspension status, prevent heavy powder deposition while retaining chemical concentration.
5 Widespread Electro-Resonance Misconceptions
Most packaging engineers resist electromagnetic upgrading due to electromagnetic interference and quality concerns, holding incorrect industry cognition:
First, electromagnetic radiation pollutes liquids. Shielded encapsulated coils release ultra-low non-ionized radiation, which cannot penetrate stainless steel nozzles, causing zero liquid contamination.
Second, resonance triggers liquid splashing. Micron-level tiny vibration generates no flow fluctuation, filling error stays within ±0.2%, meeting global metering standards.
Third, electromagnetic modules interfere with machine sensors. Independent shielding circuit isolates signal interference, compatible with original photoelectric and flow sensors.
Fourth, raise daily power consumption. Low-energy electromagnetic coils consume less than 5% extra electricity, bringing negligible operational cost increment.
Fifth, difficult daily maintenance. Sealed coil structure requires zero daily upkeep, with 3-year long service life and low replacement cost.
Low-Cost On-Site Retrofit
Factories troubled by recurring nozzle clogging can upgrade electro-resonance function with low investment, without replacing filling main units:
Install insulated annular electromagnetic coils outside existing filling nozzles, connect shielding control circuits, embed resonance linkage programs into original HMI panel, calibrate liquid-adaptive vibration parameters, and retain original pumping, metering and CIP cleaning systems. The whole renovation takes only half a working day, costs merely 5% of new filling line expenditure, and permanently solves cumulative nozzle blockage pain points.


